Company Insight
Sponsored by Sulzer
Sulzer’s AHLSTAR process pumps deliver high efficiency and wear resistance for demanding mining and minerals processing applications
In mining and metals operations, where abrasive slurries, corrosive fluids, variable ore composition, and demanding process conditions are part of daily reality, selecting the right material of construction and pumps design is a strategic decision.
Main image credit:
Reliable pumps for mines and minerals processing
Mining operations depend on reliable pumping systems to keep production moving. Whether removing groundwater from underground workings, transferring process water, or handling abrasive and corrosive process liquids, pumps must perform efficiently in some of the industry's harshest operating conditions. Unexpected failures can lead to costly downtime, production losses and increased maintenance costs, making pump selection a critical factor in achieving long-term operational performance.
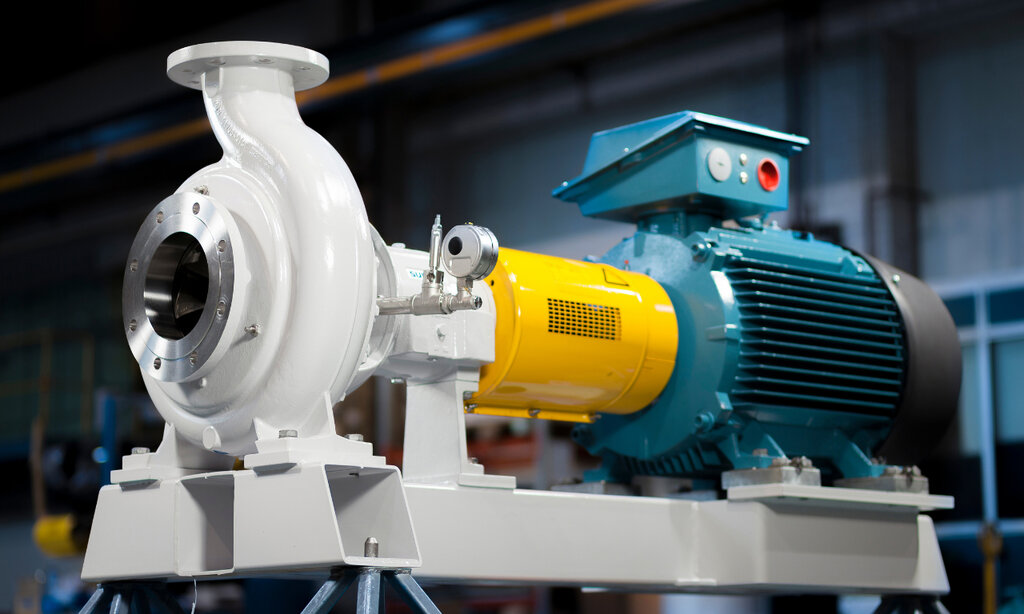
Sulzer's AHLSTAR process pump is engineered to meet these demanding requirements. Combining high hydraulic efficiency with wear-resistant design and extensive material options, the AHLSTAR range delivers reliable performance in both mine dewatering and minerals processing applications while helping operators reduce energy consumption and total cost of ownership.
Engineered for demanding mining duties
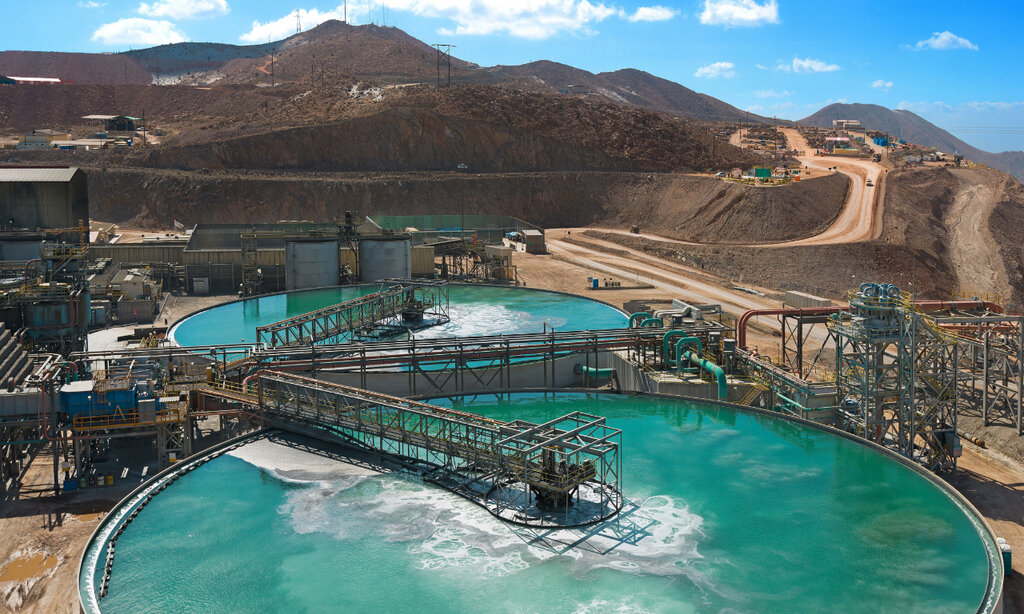
Mine dewatering presents unique challenges. Water entering underground and open-pit mines often contains fine abrasive solids, while varying groundwater chemistry can introduce corrosive conditions. On top of this, pumps must deliver consistent performance despite fluctuating flow rates, changing water levels and continuous operation.
The AHLSTAR wear-resistant process pump is ideally suited for handling contaminated mine water containing fine suspended solids, providing a highly efficient alternative where heavy-duty slurry pumps are unnecessary. Its specially designed hydraulics minimize internal wear while maintaining high efficiency, allowing operators to achieve reliable dewatering with lower energy consumption.
The same advantages extend throughout the minerals processing plant. From process water circulation and thickener duties to chemical transfer, metals leaching and refining, the AHLSTAR pump is designed to handle challenging liquids that combine corrosion with moderate abrasion. Rather than applying a one-size-fits-all approach, Sulzer selects the optimal hydraulic design and construction materials based on each customer's process conditions.
Caption. Credit:
Maximizing efficiency while reducing operating costs
Energy represents one of the largest lifetime costs of any pumping system. Even small improvements in pump efficiency can deliver significant savings over years of continuous operation.
The AHLSTAR pump is designed to operate as close as possible to its best efficiency point (BEP), maximizing hydraulic performance while minimizing energy losses. When combined with a variable speed drive (VSD), operators can further optimize pump speed to match changing process demands. This reduces energy consumption while also improving process control, decreasing component wear, and extending maintenance intervals.
Maintaining efficiency throughout the pump's operating life is equally important. Wear of hydraulic components gradually reduces head and efficiency while increasing power consumption. Regular condition monitoring and planned maintenance help restore optimal performance before excessive wear affects productivity or operating costs.
Materials engineered for corrosive and abrasive applications
Selecting the correct material of construction is just as important as selecting the right hydraulic design. In mining and minerals processing, many applications involve both corrosion and abrasion simultaneously, creating conditions that rapidly degrade conventional pump materials.
Sulzer addresses these challenges through an extensive portfolio of engineered materials, including duplex and super duplex stainless steels, highly alloyed austenitic stainless steels, nickel-based alloys, titanium, and wear-resistant cast irons. Material selection is based on a detailed understanding of process chemistry, solids characteristics, flow conditions and expected wear mechanisms.
This application expertise enables Sulzer to deliver solutions that maximize pump life while reducing maintenance requirements and replacement costs across demanding mining processes.
Caption. Credit:
Supporting lower total cost of ownership
Pump ownership extends far beyond the initial purchase price. Energy usage, maintenance, spare parts, repairs, and production downtime all contribute to the total lifecycle cost.
By combining efficient hydraulics, optimized material selection, and reliable operation near the pump's best efficiency range, AHLSTAR pumps help reduce operating costs throughout their service life. Proper pump sizing, appropriate motor selection and variable speed operation further improve overall system efficiency while reducing unnecessary wear.
These benefits allow mine operators to achieve longer service intervals, improved equipment reliability and lower lifecycle costs without compromising process performance.
Global service that keeps operations running
Reliable equipment is only part of the solution. Fast access to technical expertise and genuine replacement components is equally important for maintaining production.
Sulzer supports mining customers through its global network of service centers, providing 24/7 field service, installation support, inspections, troubleshooting, emergency breakdown assistance and root-cause analysis. Experienced field service engineers support pumps, motors, and agitators across mine sites and mineral processing plants, helping customers restore equipment quickly and prevent repeat failures.
To simplify maintenance and maximize equipment reliability, Sulzer also supplies original service kits and genuine spare parts designed specifically for AHLSTAR pumps. Using original components ensures correct fit, maintains hydraulic performance and extends equipment life while reducing the risk of unexpected failures.
Caption. Credit:
A trusted partner for mining operations
Successful mine dewatering and minerals processing depend on pumping systems that combine efficiency, durability and dependable service support. With advanced hydraulic design, engineered material selection and comprehensive lifecycle services, Sulzer's AHLSTAR process pump provides a robust and reliable solution for challenging mining applications.
Supported by global field service expertise, original spare parts and tailored maintenance solutions, the AHLSTAR range of pumps helps mining operators improve reliability, reduce downtime, lower energy consumption and achieve a lower total cost of ownership throughout the life of their pumping systems.
Read more about our AHLSTAR A process pump range
Visit the Sulzer stand at IMARC 2026 booth#L45 to learn more about our Mining solutions.
Contact information
Sulzer Australia
Rayne Cotterrell
National Sales Manager – Industry Capital Projects
Tel.: +61 447 526 485
Email: rayne.cotterrell@sulzer.com
Web: www.sulzer.com